If you're in procurement and you need ripstop nylon in volume, you know the drill. You call three suppliers, ask for price per yard and lead time, and pick whichever quote looks best. The question everyone asks is "what's your per-yard price?" The question we should have been asking is "what's actually included in that price—and what's it worth over two years?"
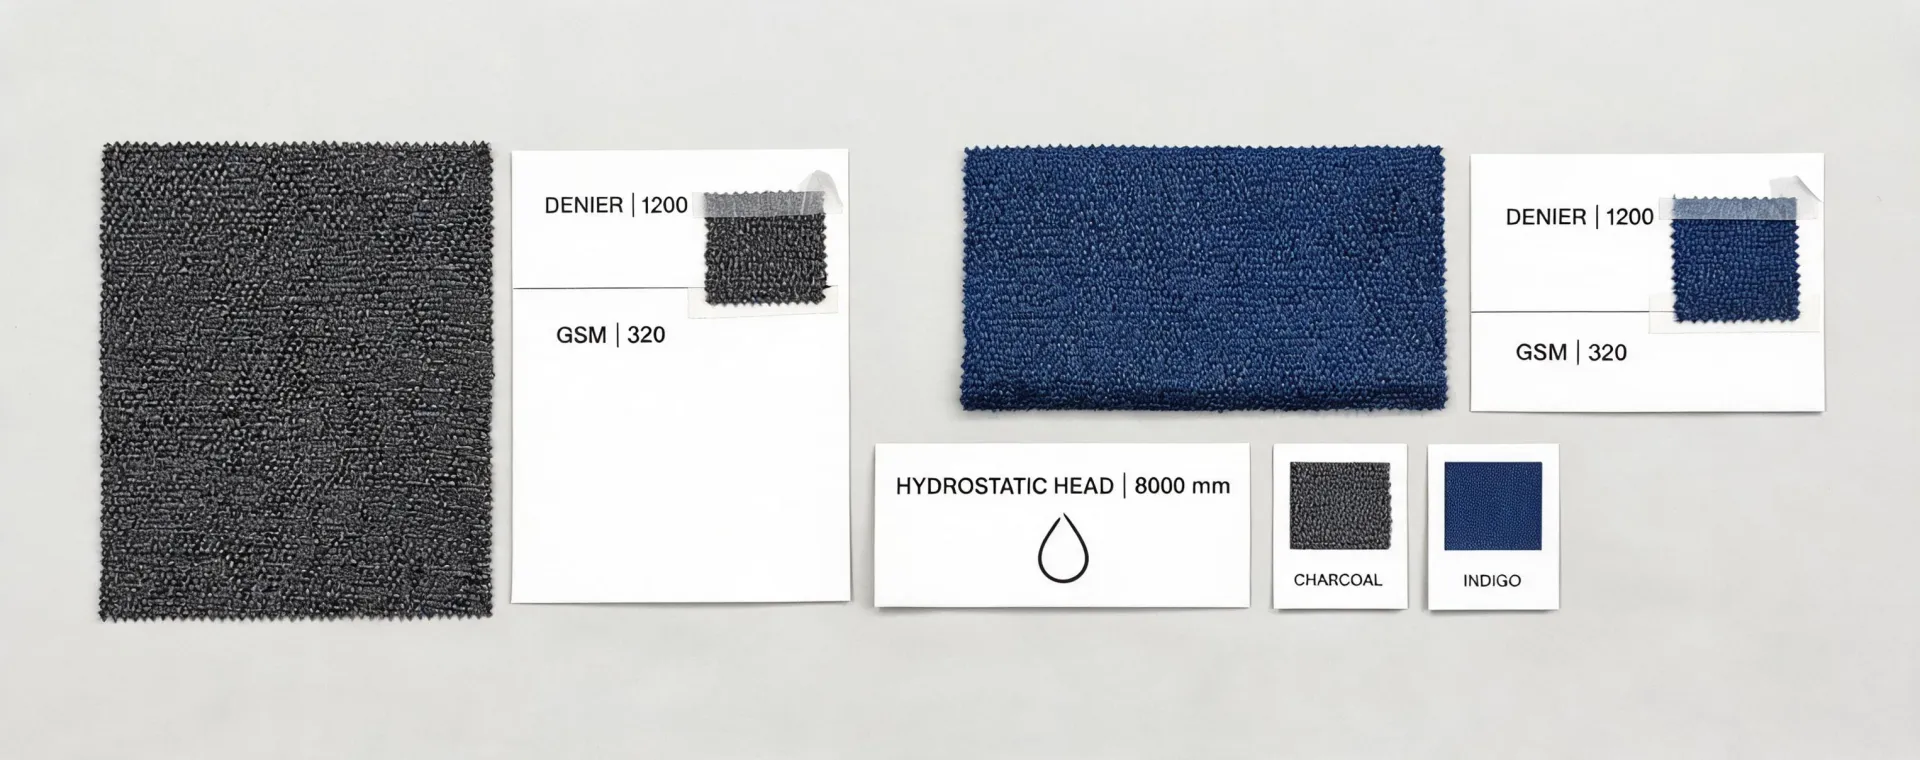
I manage purchasing for a 35-person soft-goods manufacturer in North Carolina. We make custom bags, organizers, and technical accessories for private-label brands—roughly $400K a year in fabric and trim across 8 vendors, something like 50 POs annually, and I report to both operations and finance. In 2023 we signed a contract to produce 2,000 travel backpacks for a regional outdoor brand. The spec called for 70D nylon ripstop. Simple enough, except we had to choose between stock rolls from a ripstop fabric distributor and a custom run from a technical mill like Glen Raven Custom Fabrics.
I went back and forth on that decision for two weeks. Stock was available immediately, cheaper per yard, and had no minimum-order headache. A custom run meant committing to thousands of yards of fabric before we'd sold a single backpack. On paper, stock was the safe move. My gut—plus a couple of expensive lessons from previous years—said otherwise.
The one-paragraph version: stock ripstop wins on speed and low entry cost. Custom mill fabric wins on consistency, documentation, and long-run reliability. Which one is "cheaper" depends on whether you count what goes wrong.
So here's the comparison I wish somebody had handed me, evaluated on the dimensions that actually moved the numbers: consistency, total cost, and staying in stock—plus the documentation question nobody thinks about until it's too late.
Comparison one: consistency is the brand
Our first stock order looked perfect in the swatch. The sales rep assured me it was "the same spec" as the approved sample. The first 900 yards were fine. The second lot was not. Same SKU, supposedly the same dye formula, but visibly greener under the work lights. Our lead sewer caught it before the line started, but only just barely. I stood there staring at two rolls that were supposed to match, trying to decide whether to send out a product where the front panel and the back panel didn't. (They did not match.)
We didn't have a formal incoming inspection process. When I took over purchasing in 2022, I inherited that gap, and it cost us exactly once. (note to self: photograph every incoming lot before approving.)
I'm not going to tell you stock ripstop from a distributor is bad nylon. It's not. It's just not controlled. A distributor sells you a catalog of goods from a bunch of overseas mills. Those mills are all building to a similar spec, but "similar" is doing a lot of work there. Dye lots drift. Weight drifts. Hand feel drifts.
A vertical mill is different. Glen Raven—the same company behind Sunbrella—has been running its own mills since 1880, and its Custom Fabrics division was set up for exactly this scenario: OEM and private-label brands that want a repeatable spec, not a commodity. When you buy from a place like that, you're getting a product made under one quality system, with lot-to-lot testing. You're paying for control.
And control is brand image. That backpack was going to retail for $149. The end customer had never heard of us or the mill. But they'd see, immediately, if the front panel and the back panel were two different greens. A logo doesn't fix that. Repeat customers don't come from "close enough."
The conclusion I came to: if the fabric carries your brand or your client's brand, consistency isn't a quality metric. It's the product.
Comparison two: the real cost per yard is not on the quote
Stock always wins on paper. The distributor quoted us $1.70/yard for 70D ripstop. The custom quote from the mill came in around $2.30. On 2,500 yards, that's a $1,500 gap. I'm not dismissing that.
But then the after-quote costs started piling up. We paid to return 120 yards of off-shade stock. We paid for receiving inspections and a lab test because the distributor's "test report" was essentially a re-typed sheet from their own supplier. We paid for the time our production manager spent sorting rolls by shade so the unacceptable differences stayed out of finished goods. When I totaled it at the end of the year, the cheap stock fabric had an effective cost around $2.85/yard. The custom fabric was $2.30, with zero rejected lots.
The risk went the other direction too. The upside of going custom was a consistent product. The risk was committing to 2,500 yards of fabric that would become dead stock if the client's spec changed mid-order. I calculated the worst case: a $6,000 write-off and a very awkward meeting. But then I calculated the worst case of the stock route: delayed production, rejected goods, and a client who decided our shop wasn't up to their standard. That risk was bigger.
Is custom always cheaper? No. If you need 500 yards for a one-off, custom with a 1,500-yard MOQ is silly. Stock is the answer. But if you're buying nylon fabric wholesale for an ongoing product line, the gap between "quote price" and "cost to actually use it" is way bigger than most buyers think.
The conclusion: custom costs more on the first line of the quote and less on the last line of the P&L. For anything repeatable, follow the fabric, not the price sheet.
Comparison three: availability is not reliability
Stock's biggest advantage is speed. Need 1,000 yards this week? A distributor can ship tomorrow. We've used that flexibility a ton of times.
But stock is a shared resource. When spring came—peak season for outdoor gear—the popular SKUs on the distributor's shelf were suddenly on a 3-4 week backorder. We'd planned around a 2-day lead time. That mismatch is how a purchasing manager ends up explaining to a VP why production is idle.
The custom route had a longer initial lead time. We planned 10 weeks for weaving, finishing, and testing. But once the spec was set, reorders were scheduled production, not hope. The yarn allocation is reserved. The production slot exists. Your order isn't competing with every other customer the distributor has.
This is the counterintuitive one, at least for me: the option that shipped fastest on day one was the one that left us stranded later. If you're buying ripstop once, stock wins—no argument. If you're buying it all year, "in stock right now" isn't supply reliability. It's a snapshot.
The conclusion: stock beats custom on speed. Custom beats stock on keeping a production calendar honest. Pick the one that matches how you actually buy.
The documentation dimension: nobody asks, until somebody asks
Every fabric supplier can email you a spec sheet. Very few can hand you documentation with a chain of custody.
For example, the FTC requires fiber content and country of origin on textile labels under the Textile Fiber Products Identification Act (16 CFR Part 303). That's baseline for every roll from every supplier. But when our compliance officer asked for detailed evidence—where the yarn was spun, in-house test results from the actual manufacturer—the distributor sent a one-page certificate that paraphrased their own mill's datasheet. The mill sent batch records.
That kind of traceability matters more than you'd think. We also had to be careful with the word "recycled" on a corporate order of 800 company-branded backpacks. The FTC Green Guides make clear that environmental claims need real substantiation. A mill that controls its incoming materials can answer those questions in ten minutes. A distributor would have to go ask somebody else.
If your customers never ask, this dimension is irrelevant. If they do—and corporate orders increasingly do—it picks your supplier for you.
So, stock or custom?
I'm not going to say one route is better, because it genuinely depends on your situation. Here's the decision rule I use now.
Buy stock ripstop from a distributor when:
- You're prototyping, sampling, or testing whether a product will sell.
- The order is under the custom MOQ (usually 1,000-1,500+ yards per spec).
- It's a one-time job with no likely reorder.
- Color tolerances are loose and the end product doesn't carry a premium brand name.
Go with a custom mill run when:
- The product carries a brand and the fabric is the first thing a customer touches.
- You need repeat orders that match the same standard, batch after batch.
- You project 2,000+ yards a year per spec, or 1,000+ per production run.
- You need real test data and traceability, or want to make environmental claims you can defend.
And if you're in the middle, do what we ended up doing: buy stock for the first run to get to market, and develop a custom spec in parallel. When the reorder hits, you reorder on your own spec, not someone else's catalog. You get speed today and consistency tomorrow.
Bottom line: "custom fabric" sounds like something for big brands with big budgets. In my experience, it's a different cost structure more than a more expensive one. Once shade rejects, emergency backorders, and compliance requests get added to the price of stock, the gap gets pretty small. For us, the $0.60 difference on the quote turned out to be cheap insurance—and it paid for itself in rejected lots we never had to process.